At a Glance
Conveyor Manufacturing Projects · Custom Conveyor System . Pharmaceutical Equipment . Stainless Steel Conveyor . Turnkey Project
Our client is a trusted Australian pharmaceutical and cosmetics manufacturer, recognised for producing high-quality products supported by strong regulatory compliance and technical expertise.
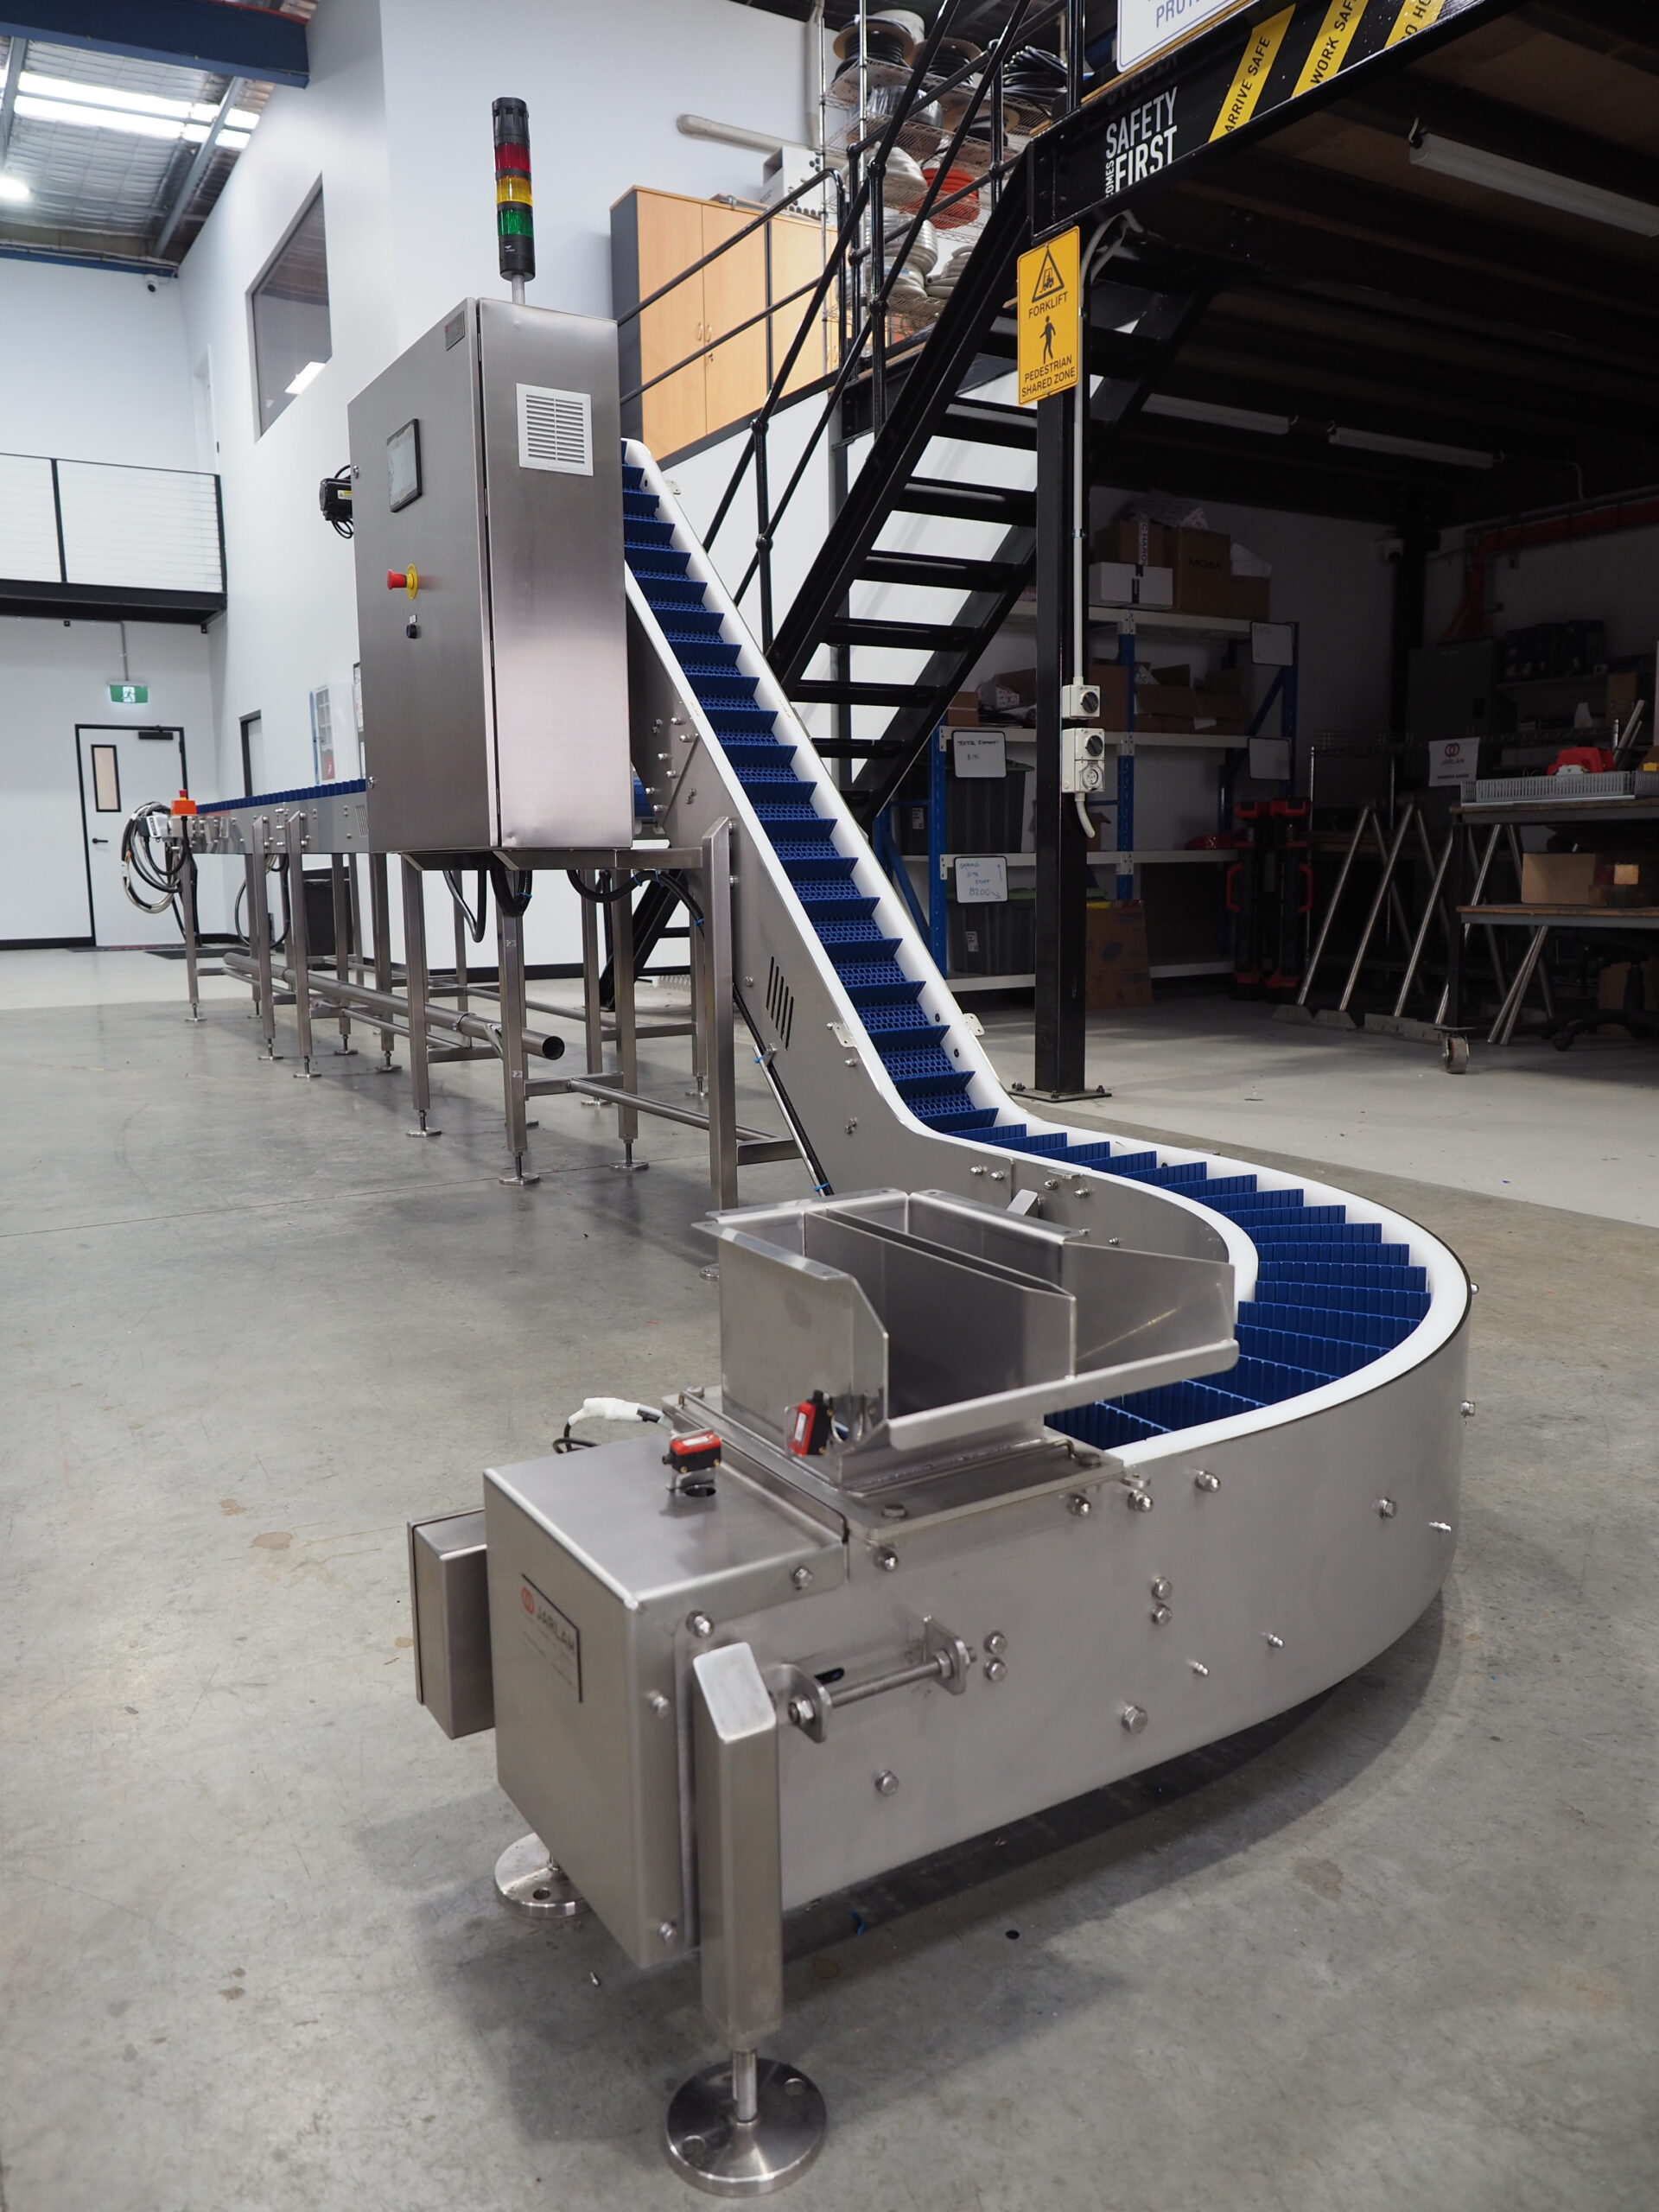
To support its production requirements, Jarlam was engaged to design, fabricate and install a customised conveyor solution that would efficiently transfer products between two production areas and integrate seamlessly with OEM equipment and machinery, creating a reliable and streamlined production process.
The Challenge:
- Enable the safe and efficient transfer of high-quality product sachets between two cleanroom production areas.
- Develop an integrated solution to accurately count, monitor and direct products into their designated containers.
- Design and manufacture a stainless steel conveyor system that meets stringent hygiene and cleanroom requirements.
- Seamlessly integrate the conveyor system with new OEM equipment and machinery to support an efficient and reliable production process.
- Provide a complete turnkey solution, with one experienced team managing the design, fabrication and installation to deliver greater efficiency and consistency throughout the project.
Our Solution:
- Designed, fabricated and installed a custom stainless steel conveyor system tailored to the client’s production requirements.
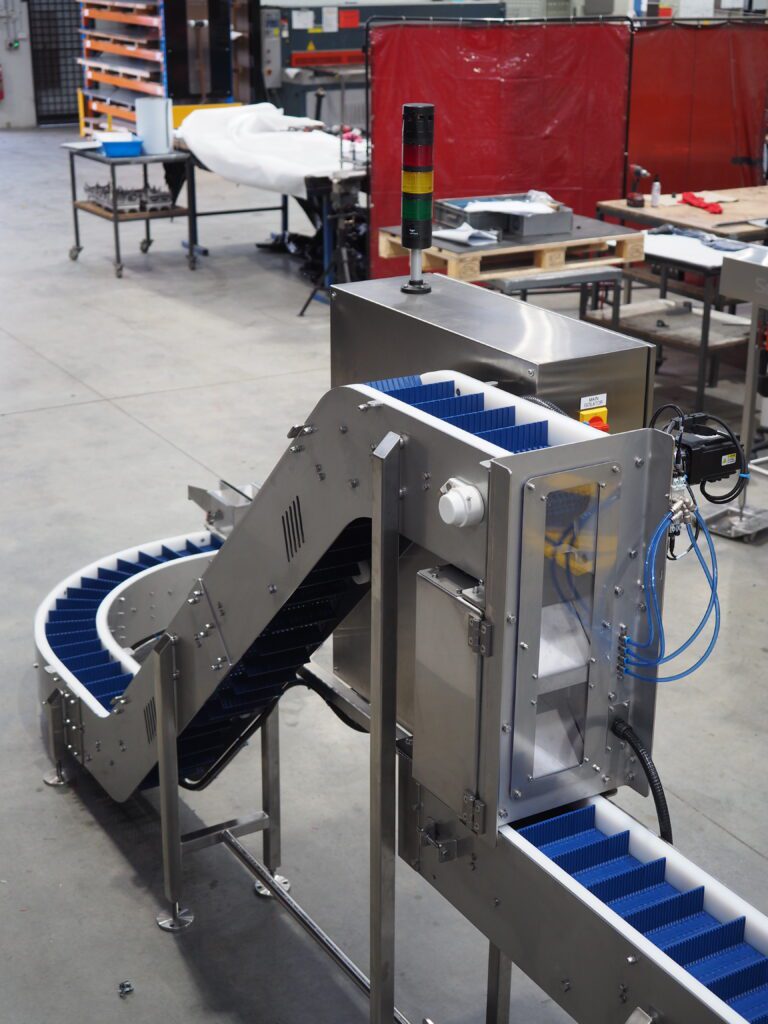
- Integrated an automated sachet counting system to accurately allocate sachets to each box.
- Engineered the conveyor system to provide the smooth and efficient transfer of products between two cleanroom production areas.
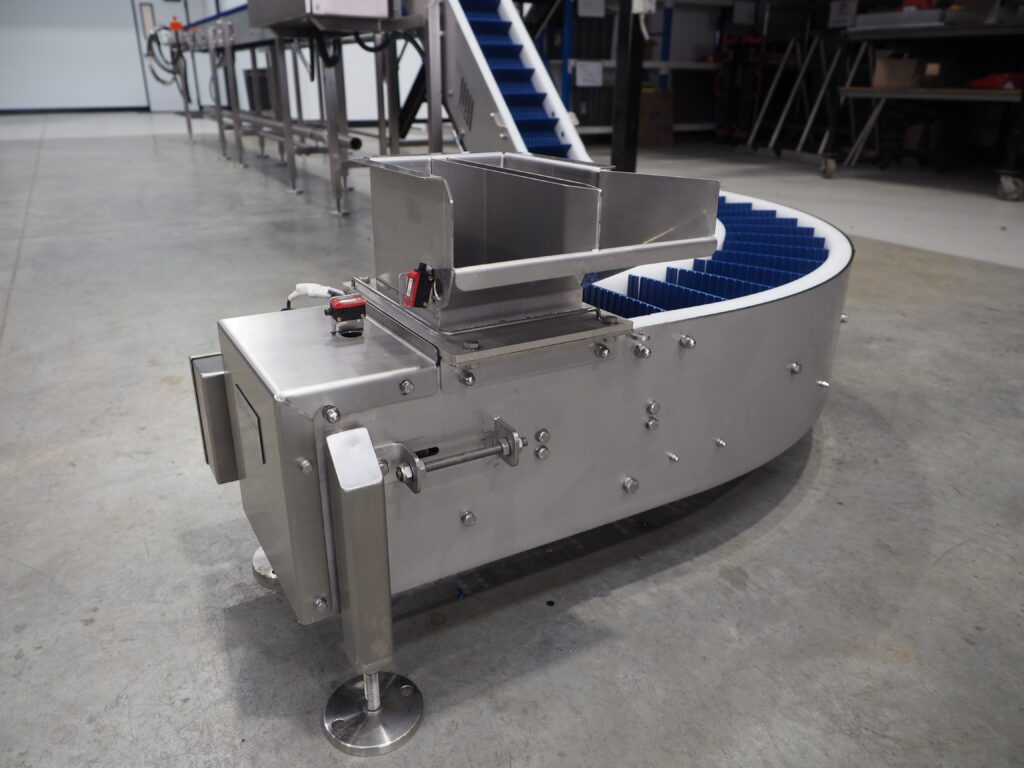
- Incorporated purpose built chutes, hoppers and equipment integrations to support controlled product flow throughout the production process.
- Incorporated a modular plastic conveyor belt specifically suited to hygienic product handling applications.
- Designed accessible, easy to clean surfaces to support stringent hygiene standards and simplify ongoing cleaning and maintenance.
- Customised the conveyor system to integrate seamlessly with the client’s existing production layout and new OEM equipment.
The Outcome:
- Increased production capacity by creating a faster and more streamlined process for transferring products between cleanroom production areas.
- Improved operational efficiency through the automation of product counting, allocation and transfer.
- Achieved greater accuracy and consistency, with the integrated counting system reliably allocating sachets to each box.
- Reduced manual handling requirements, supporting a safer and more efficient production process.
- Improved product flow through the successful integration of stainless steel conveyors, purpose built chutes, hoppers and OEM equipment.
- Reduced the risk of counting errors and product inconsistencies through the automated sachet counting system.
- Delivered a durable and hygienic stainless steel solution that supports strict cleanroom requirements while simplifying cleaning and ongoing maintenance.
- Successfully delivered a complete turnkey solution, with Jarlam managing the design, fabrication, equipment integration and installation.